Cross-contamination control in pharmaceutical manufacturing is essential for protecting product quality, patient safety, and regulatory compliance. During pharmaceutical production, materials, active pharmaceutical ingredients (APIs), microorganisms, cleaning agents, dust, or other substances can unintentionally transfer from one product, process, equipment, or area to another. If not properly controlled, this contamination can affect product quality and create significant safety risks. Effective control requires a combination of facility design, equipment controls, cleaning procedures, personnel practices, material management, environmental controls, and a science- and risk-based pharmaceutical quality system.
What Is Cross-Contamination in Pharmaceutical Manufacturing?
Cross-contamination occurs when an unwanted substance or microorganism is unintentionally transferred into another pharmaceutical product, material, process, or manufacturing area.
The contaminant may originate from:
- Previous products manufactured using the same equipment
- Active pharmaceutical ingredients
- Excipients or raw materials
- Dust and airborne particles
- Personnel
- Equipment and utensils
- Manufacturing areas
- Cleaning activities
- Air-handling systems
- Waste and rejected materials
- Inadequately controlled material movement
Cross-contamination should be distinguished from general contamination. General contamination may involve the introduction of an unwanted substance or microorganism, whereas cross-contamination specifically involves unintended transfer from another product, material, process, or source.
Why Is Cross-Contamination Control Important?
Effective cross-contamination control protects patients and maintains the quality and identity of pharmaceutical products.
Poor control can result in:
- Product contamination
- Mix-ups between products
- Microbial contamination
- Incorrect product composition
- Allergic or toxicological reactions
- Batch rejection
- Deviations and investigations
- Product recalls
- Regulatory observations
- Production downtime
- Financial losses
- Damage to product quality and company reputation
The level of control required depends on the nature of the product, manufacturing process, facility, equipment, and potential hazards.
Major Sources of Cross-Contamination
Cross-contamination can occur through several routes within a pharmaceutical manufacturing facility.
- Personnel
Personnel can transfer contaminants through:
- Hands
- Clothing
- Gloves
- Footwear
- Improper gowning
- Movement between manufacturing areas
- Poor hygiene practices
Personnel movement should therefore be controlled according to the facility’s procedures and contamination-control strategy.
- Equipment
Shared manufacturing equipment can become a source of cross-contamination when residues from a previous product remain on product-contact surfaces.
Examples include:
- Manufacturing vessels
- Mixers
- Granulators
- Tablet compression machines
- Filling equipment
- Transfer lines
- Pumps
- Hoses
- Scoops and utensils
Equipment cleaning and cleaning verification or validation are therefore important elements of contamination control.
- Raw Materials and Components
Raw materials, packaging components, and other materials can introduce contaminants if they are not properly identified, stored, transferred, or handled.
Proper material segregation, labeling, status identification, and controlled movement help minimize this risk.
- Airborne Particles
Dust generated during activities such as dispensing, milling, blending, granulation, and compression can potentially travel to nearby areas.
Airflow patterns, pressure differentials, HVAC design, filtration, and containment measures can be used to control airborne transfer.
- Facility and Personnel Movement
Uncontrolled movement of people, equipment, materials, and waste can create pathways for contamination.
A well-designed facility should consider:
- Personnel flow
- Material flow
- Waste flow
- Airflow
- Equipment movement
- Area segregation
Key Strategies for Cross-Contamination Control
Cross-contamination control requires multiple complementary controls rather than relying on a single preventive measure.
- Facility Design and Segregation
Facility design is one of the fundamental elements of contamination control.
Depending on the product and risk, controls may include:
- Dedicated manufacturing areas
- Physically separated rooms
- Controlled access
- Airlocks
- Personnel change rooms
- Material airlocks
- Appropriate pressure differentials
- Separate material and personnel flows
The appropriate approach should be determined through documented risk assessment.
- HVAC and Airflow Control
Heating, ventilation, and air-conditioning (HVAC) systems play an important role in controlling airborne contamination.
Important considerations include:
- Airflow direction
- Pressure differentials
- Air changes
- Filtration
- Temperature
- Relative humidity
- Air movement between rooms
- Recirculation arrangements
The HVAC design should prevent undesirable movement of contaminated air into areas where it could affect product quality.
- Equipment Cleaning
Cleaning procedures should remove product residues and other contaminants to an acceptable level.
A typical cleaning program includes:
- Equipment identification
- Removal of remaining product
- Initial cleaning
- Washing or cleaning with an appropriate agent
- Rinsing where applicable
- Drying
- Inspection
- Sampling or testing where required
- Documentation and release
Cleaning procedures should be validated or otherwise appropriately controlled based on the applicable requirements and risk.
- Cleaning Validation
Cleaning validation provides documented evidence that an approved cleaning process can consistently remove residues to predetermined acceptable levels.
A cleaning validation program may consider:
- Product residues
- Cleaning agents
- Microbial contamination
- Sampling locations
- Worst-case products
- Equipment configuration
- Maximum dirty hold time
- Maximum clean hold time
- Analytical methods
- Acceptance criteria
Sampling can involve techniques such as swab sampling and rinse sampling, depending on the equipment and validation strategy.
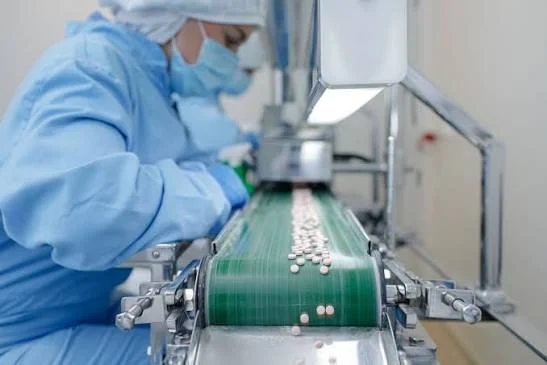
- Personnel Gowning and Hygiene
Personnel should receive appropriate training on:
- Personal hygiene
- Gowning procedures
- Hand hygiene
- Glove use
- Movement restrictions
- Entry and exit procedures
- Handling of contaminated garments
Gowning requirements should correspond to the manufacturing area and associated contamination risks.
- Material and Personnel Flow Control
Material and personnel flows should be designed to minimize opportunities for cross-contamination.
Facilities may use:
- Separate entry and exit routes
- Material airlocks
- Personnel airlocks
- Controlled corridors
- Pass boxes
- Dedicated transfer routes
- Defined waste movement procedures
The objective is to prevent uncontrolled crossing of clean and potentially contaminated flows.
- Equipment and Utensil Management
Where equipment is shared between products, appropriate controls should be established.
These may include:
- Equipment identification
- Cleaning status labels
- Dedicated utensils where necessary
- Controlled storage
- Cleaning records
- Equipment logbooks
- Preventive maintenance
- Inspection before use
Equipment should have a clearly defined status, such as clean, dirty, under maintenance, or ready for use, according to the site’s procedures.
- Dust and Powder Containment
Powder-handling operations can present significant contamination-control challenges.
Potential controls include:
- Closed transfer systems
- Local exhaust systems
- Appropriate containment
- Dust extraction
- Enclosed processing equipment
- Controlled dispensing areas
- Pressure cascade strategies
- Appropriate cleaning procedures
The controls should be selected according to the characteristics and risks of the materials being handled.
Risk Assessment in Cross-Contamination Control
A risk-based approach helps pharmaceutical manufacturers determine where stronger controls may be necessary.
Risk assessment can consider:
| Risk Factor | Example Consideration |
| Product toxicity | Potential health impact of carryover |
| Potency | Low-dose/high-potency materials may require stronger controls |
| Batch size | Influence on potential carryover |
| Equipment | Shared or dedicated equipment |
| Cleaning difficulty | Ease of removing residues |
| Solubility | Solubility of product residues |
| Dust generation | Potential for airborne transfer |
| Microbial risk | Potential for microbial contamination |
| Facility layout | Possibility of unwanted movement |
| Personnel movement | Transfer between areas |
| HVAC design | Potential for airborne movement |
Risk assessment should be documented and periodically reviewed when significant changes occur.
Cross-Contamination Control and GMP
Good Manufacturing Practice (GMP) requires pharmaceutical manufacturers to establish appropriate controls to prevent contamination and mix-ups.
A robust GMP-based approach typically integrates:
- Facility controls
- Equipment controls
- Personnel controls
- Material controls
- Cleaning procedures
- Environmental controls
- Documentation
- Training
- Quality risk management
- Monitoring and investigation
- Change control
Cross-contamination control should therefore be considered part of the overall Pharmaceutical Quality System rather than as an isolated cleaning activity.
Common GMP Practices to Prevent Cross-Contamination
Some practical practices include:
- Follow approved SOPs.
- Maintain proper personnel hygiene.
- Follow gowning requirements.
- Control access to manufacturing areas.
- Maintain appropriate material segregation.
- Use correctly identified equipment.
- Perform equipment cleaning according to approved procedures.
- Maintain cleaning records.
- Verify equipment status before use.
- Control personnel and material movement.
- Maintain appropriate HVAC conditions.
- Investigate deviations promptly.
- Implement CAPA when required.
- Assess changes through the change-control system.
- Provide regular GMP training.
Role of Environmental Monitoring
Environmental monitoring is particularly important where microbial contamination is a concern.
Depending on the manufacturing environment, monitoring programs may include:
- Air sampling
- Settle plates
- Surface monitoring
- Personnel monitoring
- Temperature monitoring
- Relative humidity monitoring
- Differential pressure monitoring
Environmental monitoring results should be reviewed for trends rather than considering individual results in isolation.
Unexpected results should be assessed according to approved procedures and appropriate investigations initiated when necessary.
Cross-Contamination vs Cross-Contact
The terms can sometimes be confused.
Cross-contamination generally refers to unintended contamination of a product or process with another substance, material, microorganism, or product.
Cross-contact is often used in the context of unintended transfer of an allergenic or sensitizing substance to another product.
The terminology and specific controls depend on the pharmaceutical manufacturing context and applicable regulatory requirements.
What Happens When Cross-Contamination Is Suspected?
When cross-contamination is suspected, the situation should be managed through the site’s established quality system.
A typical investigation may involve:
Step 1: Identify the Potential Contaminant
Determine what material, product, microorganism, or residue may have been transferred.
Step 2: Assess Affected Batches
Identify products, batches, equipment, rooms, and materials that could potentially be affected.
Step 3: Review Manufacturing and Cleaning Records
Review relevant:
- Batch records
- Equipment logbooks
- Cleaning records
- Environmental monitoring results
- Personnel records
- Material movement records
- Maintenance records
Step 4: Perform Root Cause Investigation
Potential tools include:
- 5 Why analysis
- Fishbone diagram
- Process mapping
- Risk assessment
Step 5: Implement CAPA
Corrective and preventive actions should address the identified root cause and reduce the possibility of recurrence.
Step 6: Document the Investigation
All relevant findings, decisions, actions, and supporting evidence should be documented according to the pharmaceutical quality system.
Common Causes of Cross-Contamination
Some frequently encountered causes include:
- Inadequate cleaning
- Poor equipment design
- Improper equipment status identification
- Inadequate segregation
- Uncontrolled personnel movement
- Poor material flow
- Inappropriate HVAC arrangements
- Inadequate dust containment
- Improper gowning
- Poor housekeeping
- Inadequate training
- Procedural gaps
- Failure to follow SOPs
Importantly, an investigation should establish the actual or most scientifically supported root cause rather than simply assigning blame to an operator.
Cross-Contamination Control Checklist
A practical checklist for pharmaceutical facilities can include:
| Control Area | Key Question |
| Facility | Are manufacturing areas appropriately segregated? |
| HVAC | Is airflow controlled appropriately? |
| Personnel | Are gowning and hygiene procedures followed? |
| Materials | Are materials correctly identified and segregated? |
| Equipment | Is equipment status clearly identified? |
| Cleaning | Are cleaning procedures effective and documented? |
| Validation | Are applicable cleaning processes validated? |
| Movement | Are personnel and material flows controlled? |
| Dust | Are powder-handling risks adequately controlled? |
| Monitoring | Are relevant environmental parameters monitored? |
| Documentation | Are activities properly recorded? |
| Training | Are employees trained on contamination-control procedures? |
| QMS | Are deviations, changes and CAPA appropriately managed? |
Conclusion
Cross-contamination control in pharmaceutical manufacturing requires a coordinated combination of facility design, HVAC and airflow management, equipment cleaning, personnel practices, material segregation, process controls, environmental monitoring, training, and quality-system controls. The appropriate strategy depends on the product, process, facility, equipment, and identified risks.
A strong contamination-control approach is not limited to cleaning equipment after production. It begins with facility and process design and continues through manufacturing, cleaning, monitoring, documentation, investigation, and continual improvement. By applying appropriate GMP principles and documented risk-based controls, pharmaceutical manufacturers can reduce the potential for unintended product contamination and help maintain consistent product quality.
Frequently Asked Questions
- What is cross-contamination in pharmaceutical manufacturing?
Cross-contamination is the unintended transfer of a substance, microorganism, product, or residue from one product, process, equipment, or area to another pharmaceutical product or manufacturing environment.
- What are the main causes of cross-contamination?
Common causes include inadequate cleaning, poor segregation, uncontrolled personnel or material movement, airborne particles, shared equipment, improper gowning, inadequate HVAC controls, and procedural failures.
- How does cleaning help prevent cross-contamination?
Effective cleaning removes product residues and contaminants from equipment and manufacturing surfaces before subsequent use. Where applicable, cleaning processes are validated to demonstrate their effectiveness.
- What is the role of HVAC in cross-contamination control?
HVAC systems help control airflow, pressure differentials, filtration, temperature, and humidity. Appropriate HVAC design can reduce the unwanted movement of airborne contaminants between areas.
- Is dedicated equipment always required to prevent cross-contamination?
Not necessarily. The requirement for dedicated equipment depends on the product, process, hazards, risk assessment, facility design, and applicable regulatory expectations.
- What is the role of risk assessment?
Risk assessment helps identify potential contamination pathways and determine which controls are appropriate for the specific product and manufacturing process.
- What should be done if cross-contamination is suspected?
The affected material or batch should be managed according to established quality procedures. An investigation should identify the potential source and affected areas, assess the impact, determine the root cause, and implement appropriate corrective and preventive actions.
- What is the difference between cleaning validation and cleaning verification?
Cleaning validation provides documented evidence that a cleaning process can consistently achieve predetermined acceptance criteria. Cleaning verification generally involves testing or other documented checks to confirm that a particular cleaning operation has achieved the required result.